Two roughness numbers dominate the conversation when a gas safety equipment OEM reviews a lost wax casting quote — Ra 3.2 and Ra 6.3. In this guide I will walk through what those numbers mean under ISO 1302 and ISO 8062, which detector housing geometries can ship at the as-cast finish without secondary machining, and how our Ningbo factory verifies Ra 3.2 before each shipment leaves the dock.
1. Why Ra 3.2 and Ra 6.3 are the two numbers gas detector OEMs ask about first
When a gas safety equipment procurement engineer sends our team a request for quotation, the email almost always includes one of two roughness call-outs on the drawing — Ra 3.2 or Ra 6.3. The two numbers are the most common surface-finish grades on detector housing drawings we receive, and the choice between them decides whether the as-cast finish is enough or whether secondary CNC machining has to be added to the cost line.
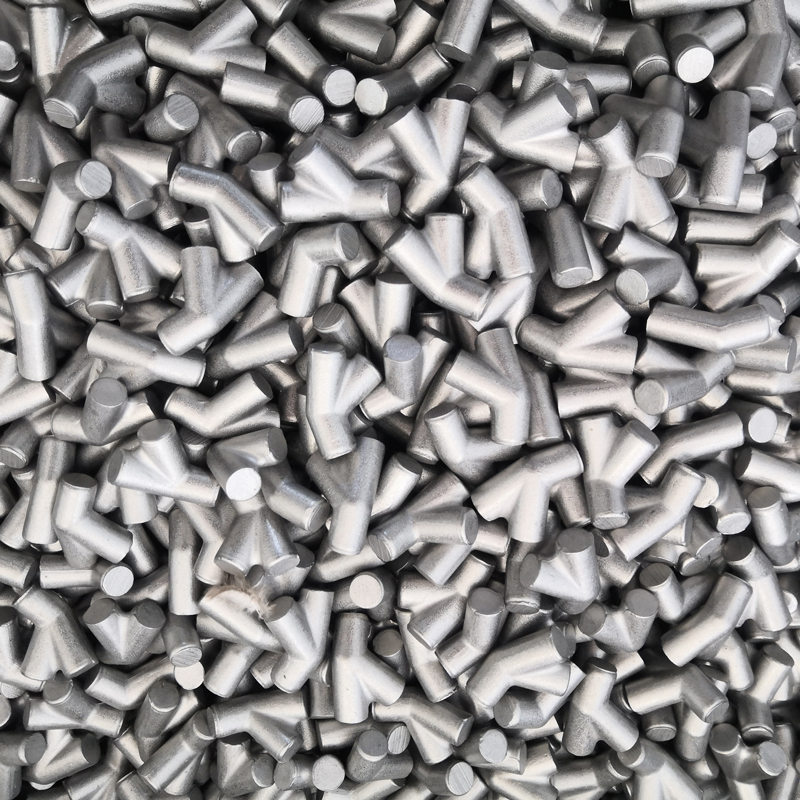
Ra 3.2 μm and Ra 6.3 μm are both standard roughness grades under ISO 1302. The grade-to-μm conversion table our team references is published by stainless-steel producer Sandmeyer Steel — stainless steel plate and pipe reference library in their technical section. Ra 3.2 is the smoother grade, and on a correctly specified lost wax casting it is achievable as-cast with a fine ceramic slurry shell and a controlled pour. Ra 6.3 is a coarser grade that typically results from a sand-blasted or pickling surface treatment. In our Ningbo production data, the typical as-cast roughness average we deliver on functional surfaces is RA 125 μin — which converts to roughly Ra 3.175 μm and falls directly on the Ra 3.2 grade. The same line, when the buyer requests a sand-blast finish for a matte appearance or for paint adhesion, lands at roughly RA 250 μin (≈ Ra 6.3 μm). We publish the RA-grade-to-μm conversion on every quote so the buyer’s drawing call-out matches our as-cast record.
Because we have run both grades for OEM buyers in the gas safety market for years, the practical question our team hears is rarely “which grade is smoother.” The practical question is “which grade lets us skip the CNC machining step on this particular housing geometry?” That is the question this article answers, using the four-factor decision matrix we built from real detector housing drawings. The matrix is part of the standard RFQ review we run for every buyer who lands on our lost wax casting parts manufacturer page.
2. What ISO 1302 and ISO 8062 CT5-CT7 mean for your casting BOM
Two ISO standards govern the conversation about lost wax casting surface finish. The first is ISO 1302, which defines the roughness-average grades (Ra 0.8, 1.6, 3.2, 6.3, 12.5, 25) and the symbol used to call them out on a drawing. The second is ISO 8062, which defines dimensional tolerance grades (CT1 through CT13) for castings. Together, the two standards give a buyer and a foundry a shared language for what the casting must look like when it comes out of the shell. The CT-grade table is also referenced by stainless-steel foundry PCFP — Pacific Coast Foundry Products, casting tolerance blog library, and by investment casting resource GIM Technology — investment casting process library. Our team cross-checks both sources during RFQ review.
For detector housings, our team works in three CT grades:
- ISO 8062 CT5 — ≈ ±0.10 mm at 10 mm nominal. Tightest practical grade for as-cast detector housings. Drives cost up and rarely needed for housing geometry.
- ISO 8062 CT6 — ≈ ±0.2 mm at 25 mm nominal. The practical working grade for most detector housing features in our experience.
- ISO 8062 CT7 — ≈ ±0.4 mm at 25 mm nominal. Looser than a sealing face should accept — the boss may not seat against the housing reliably.
The relationship between surface finish and dimensional tolerance is what matters most. A casting at Ra 3.2 as-cast finish and ISO 8062 CT6 tolerance is the pairing our buyers use most often for detector housings. Tighter CT than CT6 adds cost without adding functional value on a housing. Looser CT than CT6 starts to cause sealing and seating problems downstream. We hold our CT6 call-out on the drawing, not the foundry’s looser default, and our team flags any drawing that drops to CT7 during the RFQ review.
3. The 4-factor decision matrix — geometry, alloy, batch size, surface function
Because we receive so many detector housing RFQs each quarter, we built a four-factor decision matrix that our sales team walks every new buyer through before quoting. The matrix decides whether the as-cast finish at Ra 3.2 is sufficient or whether CNC machining has to be added. The CNC machined part after casting step is quoted separately and only when the matrix calls for it.
<>Yes — open profile, no blind pocket
| Factor | Question we ask | If YES → likely Ra 3.2 as-cast | If NO → likely Ra 6.3 + CNC |
|---|---|---|---|
| Geometry | Can the feature be reached by the ceramic slurry? | No — deep pocket, thin wall, internal channel | |
| Alloy | Is the alloy a stainless or aluminum grade we cast weekly? | Yes — 304 / 316 / A356 / A380 | No — exotic nickel alloy or copper-based |
| Batch size | Is the order 100 pieces or more? | Yes — process dialed in | No — first-article run, process not yet stable |
| Surface function | Is the surface a non-sealing, non-optical face? | Yes — outside profile, boss OD, pad face | No — sealing face, optical window seat, thread |
When three of the four factors fall into the YES column, our team quotes the housing at Ra 3.2 as-cast with no secondary CNC step. When two or more factors fall into the NO column, we add a partial-machining line item to the quote and target Ra 6.3 for the surfaces that will be re-finished by the buyer.
4. When as-cast Ra 3.2 eliminates secondary machining — 3 housing geometries
Three housing geometries sit in the YES column for all four factors and ship at Ra 3.2 as-cast in our experience. Each geometry below has shipped for gas detector or flame detector OEM buyers in the past 18 months.
Case 1 — Cylindrical sensor housing with outside profile only
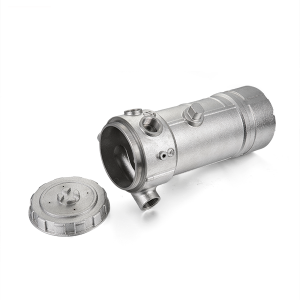
A gas detector OEM in Western Europe asked us to quote a 304 stainless steel cylindrical housing, 80 mm OD × 120 mm long, with a closed bottom and an open top for a sensor cartridge. The only critical feature was the open-top bore, and we held the bore at ISO 8062 CT6 by machining only that single face. The outside profile, the bottom face, and the four mounting pads all shipped at Ra 3.2 as-cast. The buyer saved the CNC time on five faces out of six.
Case 2 — Rectangular flame detector body with mounting flanges
A flame detector OEM in the Gulf states asked us to quote an A356 aluminum rectangular housing with four integral mounting flanges. The optical window seat and the cable gland thread were CNC machined. The four flange faces, the back cover boss, and the side pad surfaces all shipped at Ra 3.2 as-cast. The buyer saved approximately 35% of the per-piece machining time compared with a full-CNC strategy.
Case 3 — Combined UV/IR sensor housing with two cable entries
A combined UV/IR sensor OEM in Asia asked us to quote a 316 stainless steel housing with two M20 cable entries on the same face. Both cable entry threads were CNC machined. The remaining surfaces — top, sides, back, mounting feet — all shipped at Ra 3.2 as-cast. The housing carries an IP67 rating on the buyer’s incoming-inspection data.
5. When Ra 6.3 still needs CNC machining — 4 housing failure modes
Four housing geometries fall into the NO column on at least one factor and trigger CNC machining regardless of the as-cast finish. The buyer can save the machining step only by changing the geometry, the alloy, or the surface call-out on the drawing.
Failure mode 1 — Explosion-proof housing with a thread sealing face
An explosion-proof detector housing carries a thread sealing face that must seat against a gland to ATEX or IECEx certification. The as-cast finish on the thread face, even at Ra 3.2, does not meet the sealing requirement because the surface profile includes micro-peaks that create leak paths under thermal cycling. CNC machining the thread face to Ra 1.6 with a controlled surface finish is the only path. In our experience, the cost of this single CNC step is roughly 8% of the housing total — small per piece, but non-negotiable for the certification.
Failure mode 2 — Optical window seat for an IR or UV sensor
An IR or UV flame detector depends on the optical window seat holding the sapphire or quartz window at a precise stand-off distance. A surface finish rougher than Ra 1.6 at the seat creates variable optical path length and degrades the detector’s sensitivity calibration. CNC machining the seat to Ra 0.8 is the standard practice. As-cast Ra 3.2 is too rough for this application.
Failure mode 3 — UV sensor calibration drift from surface roughness
A UV flame detector calibrates against a known UV radiation source at the factory. If the housing’s internal reflectance shifts because the as-cast surface finish picks up contamination over time, the calibration drifts. A polished or machined internal surface at Ra 1.6 or better is the standard answer. As-cast Ra 6.3 on an internal sensor cavity is the wrong finish in our view.
Failure mode 4 — Gas analyzer membrane seal leak
A gas analyzer housing carries a membrane seal that must hold a pressure differential across the membrane. The seal face must be machined to Ra 1.6 with a flatness tolerance tied to the seal cross-section. As-cast Ra 3.2 is too rough for this face. CNC machining the seal face and the bolt circle is the only path we recommend.
6. How we verify Ra 3.2 in-house before shipment
Our QC team runs a three-step verification on every detector housing batch that ships with an as-cast finish call-out. The verification record travels with the shipment file so the buyer can cross-check it during incoming inspection.
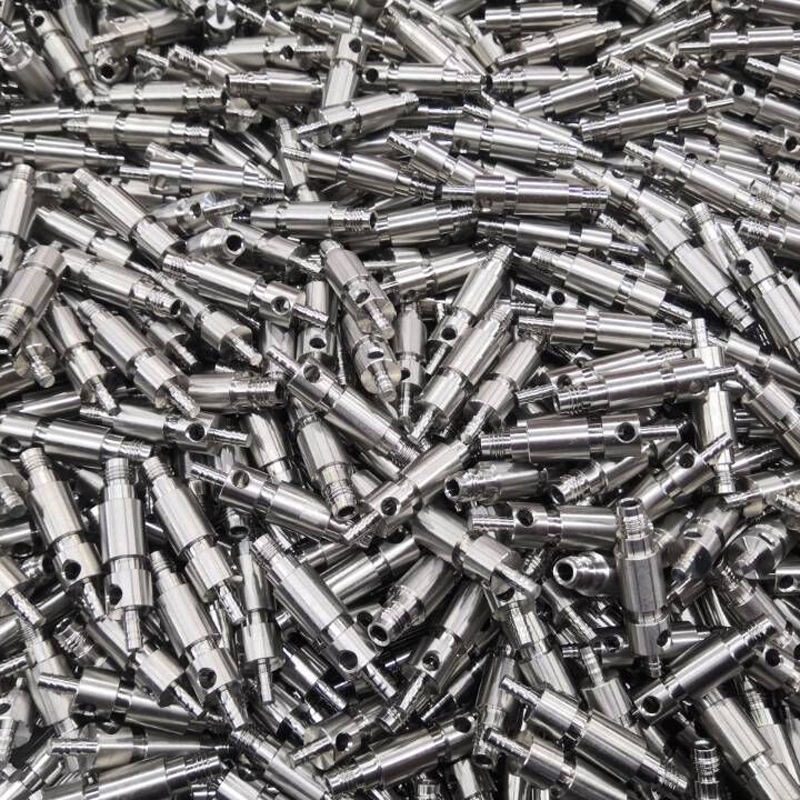
- Visual inspection against a calibrated comparator plate. Each casting is held next to a roughness comparator plate under standard workshop lighting (500 lux at the inspection desk). The QC technician grades the casting against the Ra 3.2 sample and rejects any casting that visually matches the Ra 6.3 sample or rougher.
- Sample-based profilometer measurement. At least one casting per shift per batch is measured on a portable profilometer. The measurement is taken on a functional surface in the same orientation the buyer specifies on the drawing. The result is recorded against the Ra 3.2 acceptance band.
- Drawing cross-check. Before the batch goes to packing, our QC lead cross-checks the batch record against the original drawing’s surface-finish call-out. If the drawing calls Ra 3.2 and the batch record shows Ra 6.3, the batch is held and reworked before packing.
The three steps together give our buyers a paper trail for incoming inspection. Most of the gas safety equipment OEMs we work with use the same three-step logic on their side, which is why we publish the steps in advance on every quote.
7. Five detector housing applications that benefit from as-cast finish
Five detector housing applications that we ship with an as-cast Ra 3.2 finish on at least one functional surface. Each application below uses a stainless steel or aluminum alloy per our standard detector housing material list. The full application map is published on our news page covering precision casting for gas detector machining.
- Gas detector housings. Cylindrical or rectangular bodies in 304 / 316 stainless steel. Outside profile and pad surfaces at Ra 3.2 as-cast; sealing face and cable entry at Ra 1.6 CNC machined.
- Flame detector housings (UV). Aluminum A356 or A380. Outside profile and pad surfaces at Ra 3.2 as-cast; optical window seat at Ra 0.8 CNC machined.
- Flame detector housings (IR). Stainless steel or aluminum. Outside profile and pad surfaces at Ra 3.2 as-cast; optical seat at Ra 0.8 CNC machined.
- Combined UV/IR detector housings. Stainless steel preferred for harsh environments. Both optical seats at Ra 0.8 CNC machined; remainder at Ra 3.2 as-cast.
- Gas analyzer housings. Stainless steel 316L for chemical compatibility. Membrane seal face and bolt circle CNC machined; outside profile and bracket surfaces at Ra 3.2 as-cast.
Each application sits on the same 4-factor decision matrix above. The alloy choice and the surface function factor are the two that decide whether the housing ships at Ra 3.2 as-cast or Ra 6.3 + partial machining.
8. FAQ — Six buyer questions on lost wax casting surface finish
Is lost wax casting surface finish good enough for gas detector housings without CNC machining?
In our experience, yes for a defined set of geometries. A correctly specified lost wax casting at our Ningbo facility delivers an as-cast roughness average around RA 125 μin (≈ Ra 3.2 μm) on functional housing surfaces, which meets the surface requirement for many gas and flame detector housings without secondary CNC machining. Housings with sealing grooves, optical windows, or thread seats still need CNC machining regardless of the as-cast finish.
What is the difference between Ra 3.2 and Ra 6.3 in lost wax casting?
Ra 3.2 μm and Ra 6.3 μm are both standard roughness grades under ISO 1302. Ra 3.2 is the smoother grade and is the typical as-cast roughness for shell-moulded investment castings using a fine ceramic slurry. Ra 6.3 is a coarser grade that often results from sand-blasted or pickling-finished surfaces. For most detector housing applications, Ra 3.2 is the practical working finish; Ra 6.3 usually triggers a light machining or polishing step.
Which ISO 8062 tolerance grade matches Ra 3.2 for detector housings?
For lost wax castings with Ra 3.2 as-cast finish, ISO 8062 CT6 (≈ ±0.2 mm at 25 mm nominal) is the practical working tolerance grade for detector housings. CT5 is tighter than most detector housings need and drives cost up. CT7 is looser than detector housings should accept because sealing faces will not seat reliably.
Can lost wax casting replace CNC machining for the entire detector housing?
Not for the entire housing in our view. As-cast finish works on the outside profile, the boss diameters, and the non-critical pad surfaces. The sealing face, the optical window seat, the cable gland thread, and any locating pin hole still need CNC machining because those surfaces control how the detector seals against water and dust ingress to IP65 or IP67. We always recommend a partial-machining strategy rather than full-CNC for detector housings.
Does XinYe supply OEM materials for detector housings, and what alloys are recommended?
Yes, we supply OEM and ODM detector housings through our Ningbo facility. For gas detector and flame detector housings, we typically work in 304 stainless steel, 316 stainless steel, and A356 or A380 aluminum alloys. Our gas detector reference article on the XinYe news page confirms stainless steel and aluminum as the standard housing materials for these devices.
How does XinYe verify Ra 3.2 surface finish before shipment?
Our QC team runs a three-step verification on each detector housing batch. First, a visual inspection against a calibrated comparator plate under standard workshop lighting. Second, a sample-based roughness measurement with a portable profilometer on at least one casting per batch per shift. Third, a cross-check against the original drawing’s surface-finish call-out before the batch goes to packing. The verification record travels with the shipment file.
9. Choosing Ra 3.2 as-cast versus Ra 6.3 + partial machining
Because we ship both grades from the same Ningbo line, our position is straightforward. Ra 3.2 as-cast finish is the right call for any detector housing where the four-factor matrix falls into the YES column — open geometry, standard stainless or aluminum alloy, batch size 100 pieces or more, and the surface in question is a non-sealing, non-optical face. Ra 6.3 with a partial-machining step is the right call when any of those factors flip to NO. Full-CNC on the entire housing is almost never the right call in our view — the cost is high and the functional benefit is small.
Quoting a gas detector or flame detector housing in stainless steel or aluminum?
Send our team your 3D drawing and we will run it against the four-factor matrix in this article and return a quotation with the as-cast Ra 3.2 surfaces, the partial-machining Ra 1.6 surfaces, and the per-piece price for each grade. Send your detector housing drawing to our Ningbo team.
Alison Pan — International Sales Manager, Ningbo Jiangbei XinYe Metal Works Co., Ltd.
Alison is the International Sales Manager at Ningbo Jiangbei XinYe Metal Works Co., Ltd., the Ningbo-based manufacturer behind cnnbxinye.com. The factory pairs Japanese-sourced core production equipment with a strict multi-stage quality-control program to deliver forging rings, lost-wax castings, and stamped-steel components for OEM and ODM partners worldwide. Alison works with global buyers on technical drawing review, material selection, and order scheduling, with a focus on reducing tooling iteration cycles and aligning every shipment with the buyer’s incoming-inspection plan.
Post time: Sep-15-2026